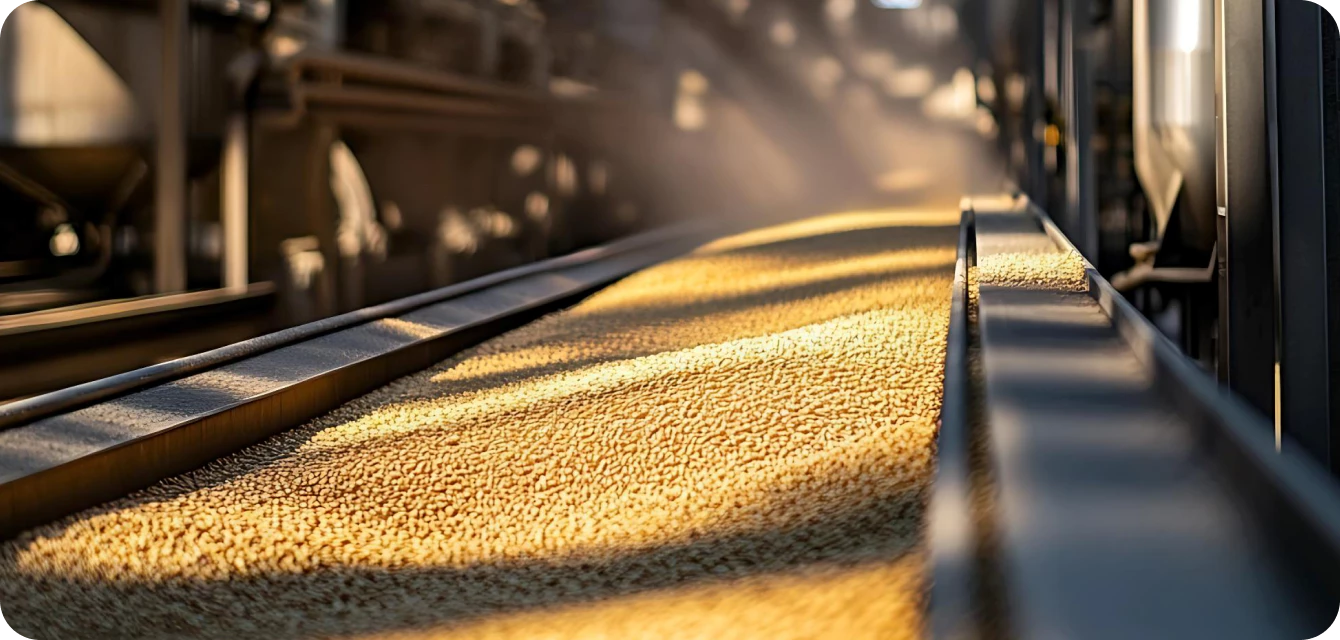
Moisture content while distillers’ grains are conveyed
Product
Online Spectral Analyzer (Reflective Version)
Deployment
Above the distillers’ grain conveyor belt
Data updates
The case describes one dataset per minute to support fermentation control
The challenge
Delayed Manual Monitoring Leads to Fermentation Instability
Traditional monitoring of distillers' grain water content relies on manual sampling, with delayed data failing to provide timely feedback on fermentation status.
Read background
Distillers' grain fermentation requires water content to be maintained between 65%-70% (too low causes substrate drying, while too high suppresses yeast activity). In conventional methods, workers take samples every two hours using a sampling spoon, weigh them, and dry them to measure water content, a process that takes three hours. One distillery failed to detect water content rising to 72% due to delayed monitoring, resulting in reduced yeast activity and a 10% drop in fermentation efficiency.
Judgment Errors Cause Alcohol Loss
Lack of precise data for controlling fermentation nodes leads to errors that impact alcohol yield.
Read background
The "optimal distillation node" for distillers' grain fermentation depends on water content (typically optimal at 68% for distillation), but traditional methods rely on experienced technicians' judgment, with deviations of 2-3 hours between technicians. In one batch, one worker judged the node at 36 hours, while another at 38 hours, causing a delayed distillation that led to alcohol evaporation and a 500kg loss in alcohol output for that batch.
Inefficient Monitoring Hinders Continuous Production Response
Manual monitoring is inefficient and struggles to meet the real-time control needs of continuous production.
Read background
Alcohol production involves continuous fermentation, processing 2 tons of distillers' grain per hour, with traditional manual monitoring conducted once every two hours, requiring six workers in shifts daily. During peak distillers' grain transfer periods, manual sampling occupies transfer time, extending monitoring intervals to three hours, making it impossible to respond promptly to fermentation changes.
How it works
Non-Contact Online Water Content Monitoring
The solution is applied to online monitoring of water content in distillers' grain, utilizing reflective spectral technology. The equipment features a non-contact design, installed above the distillers' grain conveyor belt, analyzing water content via reflective spectroscopy without touching the sticky material. It is tailored for continuous fermentation production lines in alcohol plants, withstanding the humid and warm conditions of the fermentation environment (temperature 25-35°C, humidity 80%-90%).
Precise Fermentation Node Decision Support
Provides real-time water content data to support accurate fermentation node control. Reflective spectral technology generates water content data every minute, transmitted synchronously to the fermentation control system. The interface displays real-time water content curves, automatically marking an alert line when approaching 68% (optimal distillation node), with data accuracy of ±0.5%.
Fully Automated Monitoring and Control Loop
Replaces traditional manual monitoring with a real-time response mechanism. System data directly interfaces with fermentation equipment: when water content exceeds 70%, it prompts "Increase ventilation by 10%"; when below 65%, it prompts "Activate misting for water supplementation"; and when reaching 68%, it triggers a "Prepare for distillation" signal, achieving seamless integration from monitoring to control.
What changed
Enhanced Precision in Fermentation Node Control
Improves equipment precision in controlling fermentation nodes, reducing human judgment errors. The deviation in fermentation node judgment is reduced from 2-3 hours to within 10 minutes. After implementation, one distillery saw alcohol loss due to node misjudgment drop from 3% to 0.5%.
Increased Alcohol Yield and Revenue
Boosts alcohol production efficiency and output, enhancing revenue. Precise fermentation control maintains optimal yeast activity, increasing alcohol yield by 5% (for a daily output of 20 tons, an additional 1 ton is produced daily). Fuller alcohol extraction during distillation raises single-batch yield by 8%, generating an annual revenue increase of over 200,000 USD.
Labor Reduction and Production Stability Breakthrough
Lowers manual monitoring costs and supports efficient control in continuous production. Replaces six monitoring workers, saving approximately 40,000 USD annually in labor costs. Monitoring intervals are shortened from 2 hours to 1 minute, improving response speed in continuous production by 120 times, avoiding fermentation anomalies due to delayed manual monitoring, and enhancing production stability by 40%.
Reported results describe this project and its operating conditions. Suitability for your application requires evaluation of your sample and installation.
Let's talk about your application
What would you like to measure?
You don't need a finished specification. Tell us about your sample and the problem you want to solve.
The material or sample you work with
The measurement you need
Where you plan to use it
Prefer to contact us directly?
bd@vispek.cn
International sales
+86 187 8028 5542
China sales
+86 186 6590 3209
Office
+86 755 2665 1125
Office address
Room 501, Building K, North Zone, Qianhai Shenzhen-Hong Kong Youth Innovation Hub, 5188 Menghai Avenue, Shenzhen, China